Injection Blow Moulding Machine
Scrap-free small containers with precise necks.
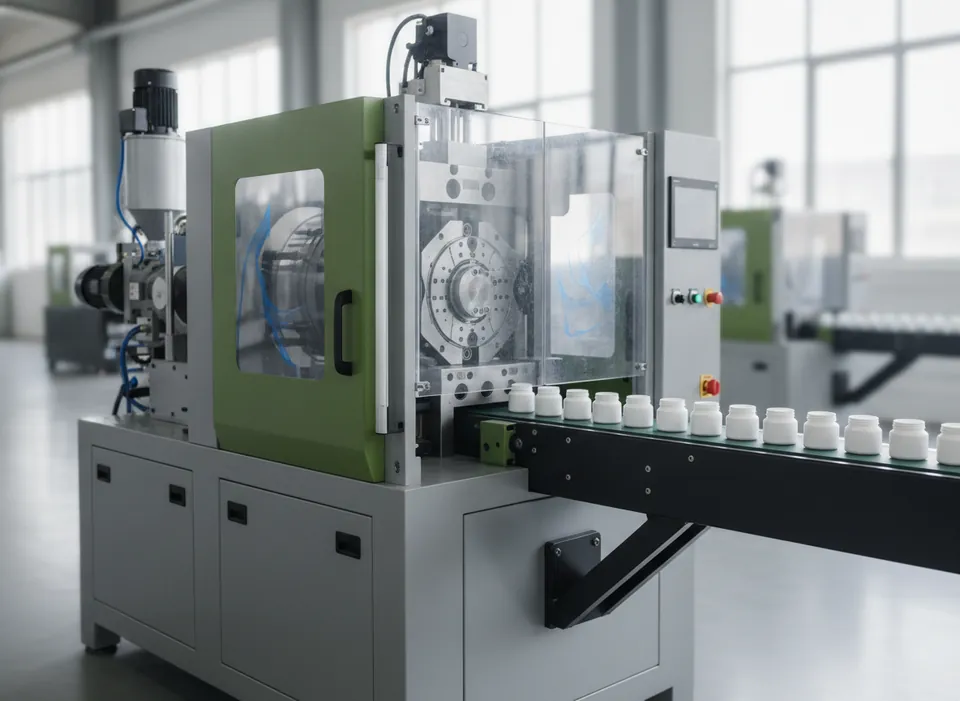
Built around your product
A three-station rotary machine injects the preform, blows it and ejects the finished container. Neck dimensions are injection-moulded, giving the accuracy that pharmaceutical and cosmetic closures require.
In extrusion blow moulding a tube of molten plastic — the parison — is captured by a mould and inflated. Stretch blow moulding reheats an injection-moulded PET preform, stretches it with a rod and blows it at high pressure, giving a strong, clear bottle. Injection blow moulding forms the neck by injection first, then blows the body, producing scrap-free containers with accurate necks.
Key features
- No flash and no trimming
- Accurate neck finish for tamper-evident caps
- Runs PE, PP, PS and PET
- Clean-room-compatible layout
Process sequence
Plasticise
Resin is melted in the extruder, or preforms are reheated.
Form
A parison is extruded or the preform is transferred to the mould.
Blow
Compressed air inflates the plastic against the cooled mould.
Cool & eject
The container sets, the mould opens and the part is removed.
Trim & test
Flash is removed and bottles are leak-tested and coded.
Machine video
A closer look at a typical blow moulding installation. Ask us for a live demonstration of the BM-I40 on your own product.
Specifications
| Model | BM-I40 |
|---|---|
| Process | Three-station injection blow moulding |
| Max container volume | 500 ml |
| Cavities | 2–12 |
| Output | Up to 3,500 containers/hour (30 ml, 10 cavities) |
| Clamping force | 400 kN injection clamp |
| Extruder / preform | Ø 40 mm screw |
| Installed power | 32 kW |
| Air supply | 0.6 m³/min at 10 bar |
Typical configuration. Final values depend on your product and are confirmed in the quotation.
Add-ons
- Parison wall-thickness control
- In-mould labelling
- Inline leak tester
- Laser coder for mould and date marking
Suitable materials and packs
Questions
Which process suits which bottle?
How are blown bottles coded?
What utilities are needed?
Get a proposal for this machine
- Application review by an engineer — material, code and line speed
- Trial marking, printing or packing on your own samples
- Quotation with layout, lead time, installation and service
Prefer to talk? Email info@motionworksrobotics.com or call +91 98100 93680.
Ask about this machine
More blow moulding machines
5 L Extrusion Blow Moulding Machine
HDPE and PP bottles and containers up to 5 litres.
30 L Extrusion Blow Moulding Machine
Jerrycans, drums and technical parts up to 30 litres.
4-Cavity PET Stretch Blow Moulding Machine
PET bottles for water, drinks, oil and personal care.